The intervention was carried out at a major Italian confectionery company located in Sicily.
The requirement concerned the cleaning of production lines from flour and sugar, food dust that, if dispersed into the environment, can create a risk of explosion and compromise the safety of the plant.
The client required a centralized system divided into three production lines, connected to a network of fixed pipes for hygienic and safe management.
Flour and sugar evoke the tradition of baking, but in the form of fine powders, they require careful industrial management. When released into the environment and reach certain concentrations, these ingredients can create hazardous conditions.
A system that aspirates flour must therefore respond to a dual requirement: keeping production lines clean and safely managing potentially combustible food dust.
The project was born from the needs of a major Italian confectionery company . The goal was to remove the buildup of flour and sugar from three production lines using a centralized, fixed, and easy-to-use system.
Why vacuum flour and sugar in production lines?
During processing, some flour and sugar inevitably settle on machinery, surfaces, and surrounding areas. As operations continue, these residues can accumulate and make cleaning the facility more challenging.
In a food service environment, order and hygiene cannot depend solely on occasional interventions . Buildup must be removed regularly through a constantly available system capable of supporting normal cleaning activities without complicating the work of operators.
Using a flour vacuum cleaner allows you to collect the deposited material without dispersing it further into the environment. Cleaning thus becomes a structured activity, integrated into the daily organization of the facility.
Flour vacuum cleaner for bakeries and combustible dust management
Flours and sugars have a dual nature. They are essential raw materials for confectionery production, but in powdered form they can behave as combustible materials. If dispersed in the air in sufficient quantities, they can contribute to the formation of explosive atmospheres.
For this reason, the choice of a flour extraction system for a bakery or confectionery factory cannot be based solely on collection capacity.
The system must be defined taking into account the characteristics of the dust and the classification of the environment in which it will be used.
The main needs of the project were closely linked:
- remove flour and sugar build-up from the lines;
- keep machinery, surfaces and surrounding spaces clean;
- safely handle combustible food dust;
- serve three distinct production lines;
- make the system easily usable by staff;
- prepare the system for possible future expansions.
Cleanliness and safety therefore become two aspects of the same process. Reducing accumulations means improving hygiene and, at the same time, limiting the presence of combustible materials in production areas.
A centralized system to vacuum three production lines
The project's complexity also stemmed from the need to address three distinct lines. The client wasn't looking for a mobile or single-point solution, but rather a centralized system capable of covering multiple work areas.
A network of fixed pipes allows the system to be permanently integrated into the plant structure. This ensures that extraction remains available throughout the production perimeter and can be used by personnel at the required locations, without having to move the entire extraction unit each time.
This configuration allows for a more orderly and consistent cleaning process in an environment where multiple lines operate in parallel. The presence of a permanent system prevents dust management from being reliant solely on localized solutions or uncoordinated interventions.
Requirements for industrial flour vacuum cleaners
Industrial flour vacuum cleaners designed for this type of application must meet specific requirements. The system required, first and foremost, had to be fixed, integrated into the plant via a permanent network of pipes.
It also needed to operate safely in the presence of combustible flours and sugars, within an ATEX-classified environment. Dust management therefore required a solution consistent with the risk conditions identified in the production area.
Another requirement was ease of use. Staff needed to be able to use the system conveniently and reliably during recurring cleaning activities, keeping lines under control without introducing unnecessarily complex procedures.
Finally, the client wanted to preserve the system's scalability. A future-proof solution can accommodate the facility's growth and the possible introduction of new extraction points.
Hygiene, safety and system rationality
The project combined three objectives: ensuring effective cleaning, properly managing combustible dust, and serving multiple lines through a single fixed infrastructure.
In this context, a flour vacuum system isn't just a simple piece of equipment for eliminating waste. It's an integral part of the production organization and helps keep the premises clean, tidy, and manageable according to plant requirements.
To find a configuration suited to your dust, line size, and area classification, contact Delfin and request an industrial extraction solution designed to meet the needs of your food processing plant.


Risk of explosion from food dust
Confectionery production involves the management of volatile ingredients that present specific challenges:
- Accumulation of residues : flours and sugars were constantly deposited along the production lines.
- ATEX Hazard : Confectionery powders are potentially explosive if saturated in air or accumulated in large quantities.
- Multi-line coverage : Need to serve three different production lines simultaneously without power losses.
- Structural requirement : Requirement for a fixed system that would eliminate the need for mobile exhaust fans between process machinery.
Centralized system certified by a third party
Delfin has implemented a centralized system configured to operate at the highest levels of safety:
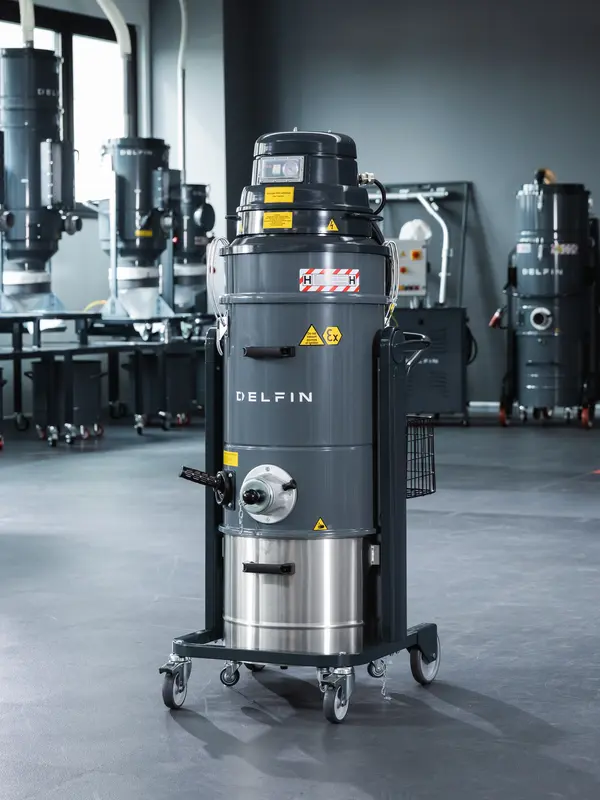
- MTL3533 EX1/3D extractor fan : fixed three-phase floor version, certified for internal zones 20 and 22 external zones, updated according to the latest safety regulations.
- Cyclonic separator : unit dedicated to the abatement and pre-separation of the material, essential for protecting the main filtering system.
- Integrated automation : 24V electrical panel with local or remote control option for total system control.
- Fixed infrastructure : connection to a fixed pipe network designed to optimize the flow rate at each suction point.
Certified safety and production efficiency
- Risk neutralization : safe management of combustible flours and sugars in full compliance with ATEX regulations.
- Filtration efficiency : the cyclone intercepts most of the material before the filter, reducing the need for routine maintenance.
- Environmental health : drastic reduction of dispersed dust, ensuring more effective cleaning of the lines.
- Scalability : centralized system that is easy to use and already set up for future expansion or integration of new lines.
Do you want to protect your confectionery production from the risk of explosive dust?
You may also be interested in